
 9


When transforming an idea, design, or prototype into a physical product, a fundamental efficiency question inevitably arises: How much of our raw material ends up as waste? What is our actual scrap rate?
If our personal engineering philosophy is built upon “minimum waste, near-zero scrap, and zero defects,” we naturally set the bar at the absolute peak to stand behind our work. The product must perform its promised function flawlessly, raw materials must not be wasted, and every conceivable user-induced error must be anticipated before the product ever reaches the market.
However, this pursuit of “absolute perfection” introduces a dangerous paradox in manufacturing practice: The risk that the product never ships at all due to the uncompromising quality and zero-scrap standards we impose on ourselves. While we spend weeks at the drawing board trying to squeeze another two percent out of a cutting layout (nesting) or perfecting an enclosure, we look out at the market and see competing products—often far less efficient, poorly ergonomic, and clearly built with a “fix it on the fly” iterative mentality—being sold, used, and updated version after version.
So how does the global industry handle this? What is the globally accepted “efficient” scrap rate in manufacturing? Let us examine this dilemma through both physical/mathematical laws and time and engineering economics.
1. The Physical and Mathematical Limit: Why Scrap Can Never Be Zero
No matter how skilled we are as designers or engineers, two unyielding physical and mathematical walls stand in the way of achieving zero material scrap:
A. The Lagrange-Thue Circle Packing Theorem (The Geometric Limit)
Imagine cutting circular or curved components out of a flat rectangular sheet of fabric, paper, acrylic, or sheet metal. No matter how tightly you arrange the parts, geometric gaps will remain between them.
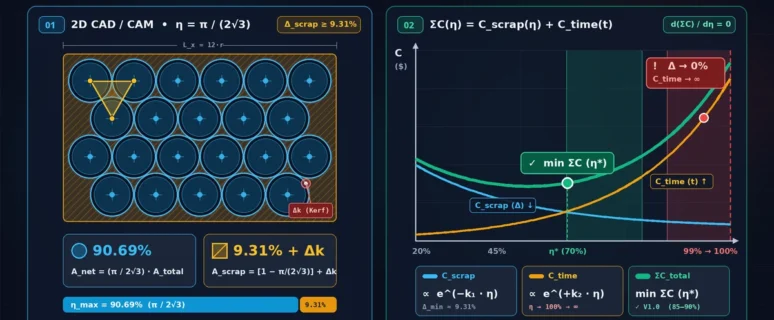
According to the Circle Packing Theorem, proven by mathematicians Joseph-Louis Lagrange (1773) and Axel Thue (1890), even if you arrange identical circles in the densest possible hexagonal (honeycomb) lattice across an infinite flat plane, you can cover at most 90.69% (η = π / (2√3) ≈ 0.9069) of the surface area. The remaining 9.31% is mathematically mandatory scrap. If you arrange those same circular parts in a standard square grid instead of a hexagonal lattice, the mandatory geometric waste jumps to 21.46% (1 − π/4).
B. Tool Kerf and Process Margins
When a laser beam, cutting blade, or CNC end mill cuts through material, it vaporizes or turns into chips a volume of material equal to its own physical width (kerf loss). Furthermore, gripping margins required to keep the sheet from shifting on the machine bed, printing bleed areas, and optical registration marks (fiducials) are mandatory material sacrifices required to guarantee the dimensional accuracy of the final product.
2. Globally Accepted Industry Scrap Rates
In industrial engineering and cost accounting, material waste is divided into “Normal (Unavoidable) Scrap” and “Abnormal (Preventable) Scrap.” Globally, “efficient manufacturing” does not mean zero waste; it means operating within the following established industry tolerance bands:
| Manufacturing / Processing Method | Accepted Normal Scrap | Best Practice (Optimum) | Primary Source of Scrap |
| 2D Flatbed Cutting (Fabric, Felt, Leather, Paper, Sheet Metal) | 12% – 25% | 8% – 12% | Interstitial gaps from irregular pattern nesting on rectangular sheets and perimeter clamping margins. |
| Printing, Labels, and Carton Packaging | 4% – 8% | 2% – 4% | Print bleed margins, optical registration marks (crop marks), and initial machine calibration sheets. |
| Molding and Casting (Injection, Resin/Polyester) | 2% – 6% | 1% – 2% | Mold sprues and runners, air vent flash, and initial thermal/pressure stabilization shots. |
| Wood and Panel Sizing (CNC Router / Panel Saw) | 10% – 20% | 7% – 10% | Cutting tool thickness (kerf), panel edge trimming allowances, and grain-direction constraints. |
| Subtractive Machining (Metal CNC Milling / Turning) | 30% – 60% (Gross) | 2% – 5% (Net) | High chip volume as parts are carved from solid billets; however, metal swarf is recycled, keeping net financial loss low. |
| Additive Manufacturing (3D Printing) | 3% – 10% | 1% – 3% | Breakaway support structures, bed adhesion perimeters (brim/skirt), and purge/calibration towers. |
3. The Economics of Quality: Juran’s Curve and the Taguchi Loss Function
Why does striving for zero scrap and zero defects become counterproductive past a certain point? Two pioneers of quality engineering answered this question decades ago:
Juran’s Optimum Cost of Quality Model (Law of Diminishing Returns)
In his foundational Quality Control Handbook, Joseph M. Juran analyzed the economics of reducing defects and material waste, revealing a striking curve:
- Reducing scrap from 25% down to 10% is straightforward and yields immediate, substantial material savings.
- Reducing scrap from 10% down to 5% requires solid engineering planning and pays off well for the effort invested.
- However, the moment you attempt to push scrap from 5% down to 0% (or eliminate every conceivable edge-case defect), Design, Prevention, and Time Costs skyrocket vertically toward infinity (∞). You end up spending $1,000 worth of engineering time, mental energy, and R&D to save $10 worth of raw material.
The Taguchi Quality Loss Function
Japanese engineer Genichi Taguchi defined quality not as “abstract perfection,” but as “minimizing the total loss a product imparts to society and the production system.” Viewed through Taguchi’s lens, when an engineer delays a product for months to shave off a few percent of scrap or preempt every hypothetical user error, it destroys 100% of the utility the product would have provided to users—representing the largest possible quality loss.
📊 Interactive Simulation: Balancing Material Scrap vs. Engineering Time Cost
Use the interactive simulator below to select a manufacturing process and adjust the Zero-Scrap & Perfection Effort Level. Observe how material scrap cost intersects with engineering time cost, and see where the “Economic Optimum” transitions into the “Perfection Trap”:
⚙️ Juran Cost of Quality & Scrap Simulator (e-zeka.net)
Select a manufacturing method and slide the optimization effort to explore the trade-off between material scrap and engineering time cost.
4. Why the "Fix It on the Fly" (Iterative) Approach Wins
The reason competing products with lower material efficiency or less refined ergonomics succeed in the market comes down to Iterative Development (Versioning) and the Pareto Principle (The 80/20 Rule):
- Laboratory Blindness: At the design desk, you can only predict a fraction of real-world user errors. Actual user behavior is chaotic; trying to eliminate 100% of user errors before launch means spending months engineering safeguards for scenarios that may never happen in reality.
- The Real Scrap is Time, Not Material: When you shelve or delay a project for months to avoid a 5% material scrap rate, you actually incur a 100% scrap rate on your time, mental energy, and existing prototype materials. The most expensive waste in manufacturing is not the offcut in the bin—it is the unshipped idea.
| Comparison Criterion | Absolute Perfection ("Zero-Scrap") Approach | Industrial / Iterative Optimum Approach |
| Material Scrap Target | Convergence to 0% (Maximum raw material conservation). | Industry-accepted "Tolerance Band" between 5% and 15%. |
| Time & Effort Scrap | Extremely High (80% – 100%). All design time becomes idle waste if the product never ships. | Low. Design time is time-boxed; concepts rapidly convert into shippable output. |
| Definition of Quality | Flawlessness; preempting every possible user mistake prior to release. | Reliability; ensuring the product delivers its core promised function dependably. |
| Standing Behind the Product | "Never releasing a product until it has zero flaws." | "Shipping a solid V1.0, standing behind it in the field, and evolving it into V2.0 with real data." |
5. Conclusion: 3 Engineering Rules to Ship Your Product
To turn your designs into finished products without compromising your integrity as a creator, reframe your quality standards around three actionable engineering rules:
- Establish an "Acceptable Scrap Allowance": Before starting a job, accept a natural scrap rate based on the medium (e.g., 12–15% for 2D sheet cutting, 5% for printing) as a standard cost of doing business, just like electricity. If trying to beat that percentage takes more than 30 minutes of layout tweaking, stop optimizing and start cutting.
- Separate "Core Function" from "Secondary Polish": To stand behind your product, Safety and Core Function (the primary job promised to the user) must work at 100%—never compromise there. However, for Material Nesting Efficiency and Secondary Ergonomic Details, accept 85% as your "V1.0 Release Threshold."
- Reframe Offcuts as "Calibration & Test Stock," Not Waste: By setting aside perimeter offcuts for machine calibration, test cuts, or smaller auxiliary parts on future jobs, you remove the psychological pressure of "wasting material" and free yourself to move swiftly into production.
📚 Academic & Industrial References
- Lagrange, J. L. (1773). Recherches d'arithmétique. Nouveaux Mémoires de l'Académie Royale des Sciences et Belles-Lettres de Berlin. (2D Lattice Packing Density:
π / (2√3) ≈ 0.9069). - Thue, A. (1890 / 1910). Über die dichteste Zusammenstellung von kongruenten Kreisen in einer Ebene. Norske Vid. Selsk. Skr., No. 1, 1–9.
- Juran, J. M. (1951). Juran's Quality Control Handbook. McGraw-Hill Education. (Cost of Quality Model & Economic Optimum Curve).
- Taguchi, G. (1986). Introduction to Quality Engineering: Designing Quality into Products and Processes. Asian Productivity Organization.
- Horngren, C. T., Datar, S. M., & Rajan, M. V. (2015). Cost Accounting: A Managerial Emphasis. Pearson. (Accounting Standards for Normal vs. Abnormal Spoilage/Scrap in Manufacturing).